Cosmetic Bottles Factory Quality Standards Every Beauty Brand Should Check
2026-11-20
Most beauty brands obsess over formula, shade, and campaign aesthetics—but the bottle is what customers actually touch first. Factory quality standards are where great packaging either holds up or quietly falls apart: a loose cap, a cloudy finish, a pump that jams after three uses. Before you commit to a supplier, it helps to know the specific checks that reveal whether a cosmetic bottle will protect your product or damage your reputation. At Zhejiang Haitong Plastic Industry Technology Co., Ltd., those standards shape everything from raw material selection to final inspection. Here are the ones beauty brands rarely ask about until something goes wrong.
The Leachables Check Most Brands Skip
Most brands stop at extractables testing under exaggerated conditions and call the job done. That misses the real question: what actually migrates into the formula during normal storage, repeated use, and long-term contact with a drug product or food. Leachables are the substances that end up in the final matrix, and they don't always match the extractables profile. Heat, light, pH, and the product's own chemistry can pull out additives, stabilizers, breakdown products, or unexpected reaction byproducts that a standard screen never targets.
The reason this check gets skipped isn't usually ignorance. It's cost and time. A meaningful leachables study requires realistic conditions, multiple time points, and sensitive methods that can identify unknowns at very low levels. Plenty of manufacturers rely on generic material certifications or pass-through claims instead of testing the finished system under conditions that reflect actual use. That leaves a blind spot where a container, gasket, tube, or label can quietly release something into the product after months on the shelf.
A stronger approach treats leachables as a product-specific risk rather than a box to tick. It looks at dosage form, route of administration, patient population, and the full contact system. From there, thresholds and analytical methods can be matched to what the product actually needs. The brands that do this well usually end up with cleaner change control too, because they know which components matter and which substitution could alter the leachables profile.
Cap Liners That Fail Only After Filling
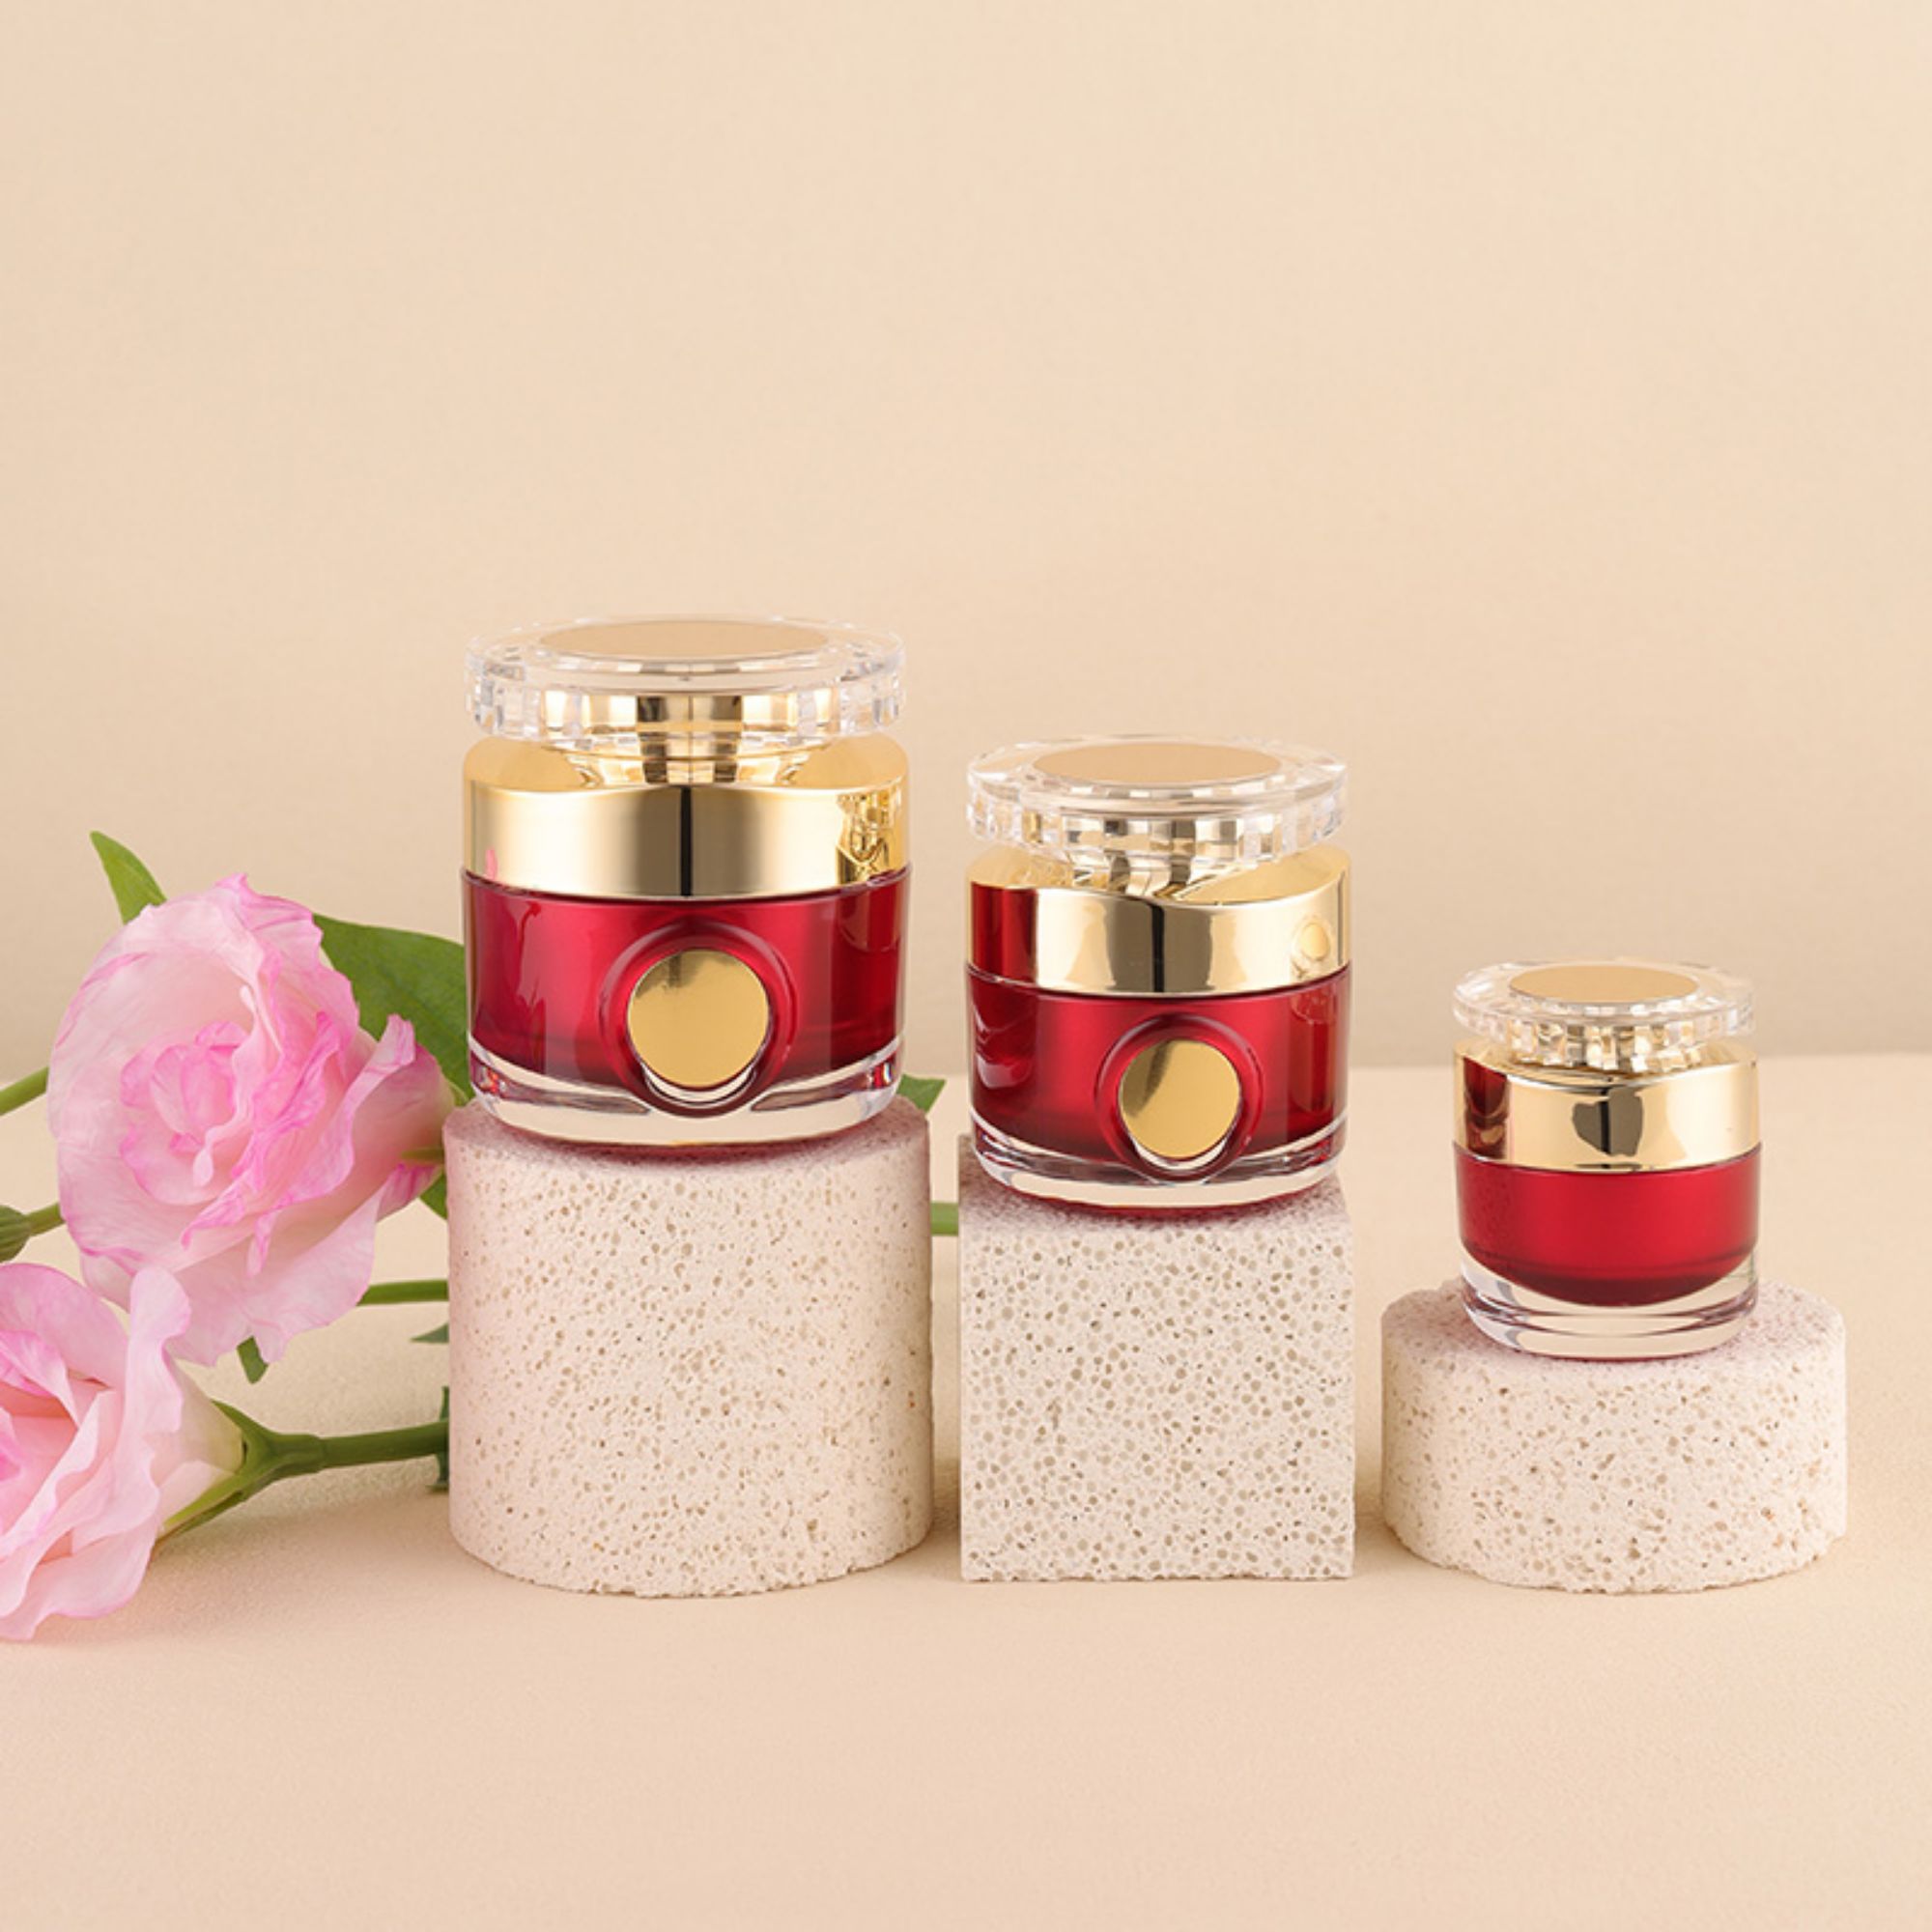
Most liner problems show up before the cap ever reaches the filler. What makes this failure mode different is how ordinary the first inspection looks. The liner sits flat, the cap torques to spec, and a dry cap check passes without any visible flaw. The trouble begins once product splashes onto the sealing surface or the bottle cools after hot filling. That is when the backing can start to lift, the seal can micro-channel, or the adhesive can soften just enough to lose contact.
On a filling line, this often appears as intermittent leakers that cannot be reproduced with empty bottles. Operators may blame cap application torque or capping head alignment, but the real variable is how the liner reacts to the filled environment. Oils, surfactants, alcohol, and acidic products are especially good at finding weak edge seals that a dry cap never exposes. A liner that survives a two-second dry pull test may still creep or wrinkle after thirty minutes of contact with the product.
The most reliable way to catch these delayed failures is to test liners in the actual fill environment, not just on a dry capper. That means running filled stability samples, checking seal appearance after a set contact time, and tracking torque retention on stored packs. If a liner only fails after filling, changing the liner film, wax layer, or pulp backing often resolves the problem faster than chasing downstream cap adjustments.
Why Bottle Tolerances Decide Your Line Speed
Bottles are not just containers on a high-speed line; they are mechanical components. Every star wheel pocket, timing screw flight, and gripper is machined around a nominal dimension. When the tolerance band drifts, the transfer points no longer match. That mismatch shows up as tipped bottles, scuffed labels, or a filler tube snapping a neck finish. The line does not care about your production target; it reacts to the physical reality of the bottle in front of it.
A neck finish that varies by a few thousandths may not look like much on a spec sheet, but at 30,000 bottles per hour it changes how the capper chuck seats. Operators then slow the filler or capper to keep reject rates acceptable. The same applies to body diameter and overall height. If the base is slightly out of round or the height stacks at the upper limit, the star wheel can pinch the bottle, and one jam cascades into a full conveyor stoppage.
Tight tolerances give you the freedom to raise speed without raising chaos. Loose tolerances force the line to run at the pace of the worst bottle in the batch. That is why buying cheaper preforms or pushing a mold past its maintenance window usually costs more in lost throughput than it saves in material. Match the bottle geometry to the transfer points, and line speed stops being a guessing game.
Coatings That Look Great Until the First Alcohol Wipe
The first time you run an alcohol wipe across that sleek matte surface, it feels almost like a betrayal. The coating looked bulletproof in the showroom, and now it's streaking, clouding, or peeling away in sticky ribbons. Most people assume they got a defective batch, but the truth is more mundane: many modern finishes are tuned for visual appeal and dry abrasion, not chemical resistance. Alcohol in particular is a solvent that loves to creep under the edges of lightly cross-linked polymers, lifting them from the substrate before you even notice the damage.
What makes this so frustrating is how invisible the vulnerability is until the exact wrong thing touches it. Isopropyl alcohol at 70% concentration is standard for cleaning screens, hand oils, and even minor scuffs, so it shows up everywhere. Yet the same coating may survive hundreds of rubs with a dry cloth or even mild soapy water. The failure isn't linear — it's a threshold effect. Once the alcohol breaks the surface tension and starts swelling the top layer, each subsequent wipe digs a little deeper, turning a once-uniform finish into something that looks like a cracked desert floor. By the time you notice the haze, the damage is frequently irreversible without a full refinish.
If you want to avoid this trap, stop relying on marketing terms like "scratch-resistant" or "durable." Ask instead what the coating does when it meets common solvents. A quick test on an inconspicuous corner with a cotton pad and 70% isopropyl alcohol will tell you more in thirty seconds than any spec sheet. And if you already own something that has lost the fight, don't keep wiping — an alcohol-based cleaner only accelerates the breakdown. Switch to a dry microfiber or a very dilute, pH-neutral solution, and accept that some appearances were never meant to survive real-world chemistry.
Transit Testing Without the Polished Lab Demo
Real transit testing rarely looks like the tidy setup shown in a lab walkthrough. It starts with a pallet strapped to the floor of a box truck, a few borrowed accelerometers, and someone checking zip ties at a loading dock while it starts to rain. By the time the truck hits the first rough stretch of highway, one logger has already shifted, and the only thing you know for certain is that the packaging is getting a harder workout than the demo suggested.
The absence of a polished demo changes what you measure. There is no controlled sine sweep or neatly staged drop sequence; there are potholes, hard braking, and a forklift operator who sets the pallet down faster than the spec allows. The resulting data is messy and often embarrassing, but it shows which failures repeat under ordinary abuse. That matters more than a clean graph produced on a test bench.
A useful transit test under these conditions comes from doing less, not more. Pick a short route with familiar road surfaces, run it three times with the same load, and only treat consistent damage or consistent signal spikes as real findings. If a bracket bends on every trip, the fix is obvious. If it survives the ugly, unscripted run, it has a much better chance of surviving the actual supply chain.
Traceability That Survives a Real Recall
Most traceability plans look flawless until a contaminated lot actually ships. Then the gap between what a spreadsheet promised and what a warehouse remembers becomes expensive. A recall that survives contact with reality depends on records that capture movement as it happened, not as it should have happened. Lot codes, rework, repacking, partial returns—these ordinary events break traceability quietly.
In a real recall, the goal shifts from having data to narrowing the scope before regulators and customers lose patience. Teams that can trace a single batch through every handoff, including samples, substitutions, and rejected material that got reintroduced, can pull affected product in hours. Teams that cannot end up widening the recall to cover uncertainty. That distinction is rarely visible in an audit but becomes obvious when trucks are already unloading at retail.
The systems that hold up tend to be deliberately simple. One code stays with the product, even when it is split or blended. Someone owns the record at each transfer. Paper and scanners work together instead of competing. The point is not collecting more data; it is keeping the data connected to physical movement. A recall is just the moment that connection finally matters.
FAQ
Ask to see incoming resin certificates and batch traceability before looking at samples. If the factory cannot link the lot numbers on raw material documents to finished bottles, that is a red flag, even if the showroom looks impressive.
Measure the shoulder, base corner, and the area just below the threads, not the middle of the bottle. Ask for per-cavity readings. A factory that only gives you one averaged number is probably hiding inconsistency.
Vacuum decay is more dependable than an old-fashioned water bath for slow leaks. After capping, ask for vibration testing followed by negative pressure. Also make sure the liner still seals after the cap has been opened and closed several times.
Put the actual formula in contact with the bottle, liner, gasket, and pump or dropper at around 40 to 50 degrees Celsius for four to eight weeks. Watch for stress cracking, color shift, weight loss, and changes in viscosity or pH. A generic plastic compatibility chart is not enough.
Request tape adhesion, alcohol rub, sunscreen contact, and UV aging tests on printed or hot-stamped surfaces. The real issue is whether the decoration survives normal bathroom use, not how it looks fresh out of the box.
Lock down neck finish diameter, thread dimensions, height, overflow capacity, and sealing surface flatness. Neck diameter tolerances around plus or minus 0.2 mm are common. The bottle and closure should be approved as a pair, because individual part drawings can miss fit problems.
A batch inspection report covering dimensions, capacity, seal performance, color difference, and cosmetic defects. Request material compliance statements and any food-contact or heavy metal test reports. The lot numbers on the documents should match the carton labels exactly.
It usually comes from multi-cavity tool variation, inconsistent regrind percentage, or uneven cooling. Ask the factory to mark cavity numbers and sample each cavity. If the color difference is above about delta E 1.0, it is likely visible to the eye and worth rejecting or sorting.
Conclusion
Most beauty brands still treat bottle qualification as a quick visual sign-off, but the real problems sit where packaging meets formula. Leachables testing is rarely extended to actual filled product stored under temperature swings, so a bottle that passes a water-based blank can still shed antioxidants or slip agents into an oil serum after eight weeks. Cap liners are just as deceptive: they seal fine during a short trial, then swell, wrinkle, or delaminate once the filling line torque and the product's fragrance load have had time to work. Dimensional tolerances are not only about leaks. Slight neck finish drift or uneven base flash can turn a supposedly high-speed run into continuous stoppages, jamming unscramblers and messing with capping torque.
Surface finishes need abuse testing that reflects actual use, not a polished demo bottle handled with gloves. A coating can pass inspection and still cloud, peel, or tack up after contact with alcohol, hand cream, or sunscreen residue. Transit testing should involve real cartons, mixed pallet weights, and unrefrigerated truck conditions rather than a tidy lab drop test. And when something does go wrong, traceability has to reach beyond a batch number on a carton. Factories should be able to trace a single bottle back to the resin lot, the cavity number, the liner material, and the filling shift without relying on a spreadsheet that falls apart under recall pressure.
Contact Us
Contact Person: Kara Yang
Email: [email protected]
Tel/WhatsApp: 8618857568397
Website: https://www.haitongplastic.com/