Optical Slip Ring Company Insights for Reliable High-Speed Rotational Connectivity
2026-09-27
Every millisecond counts when your system spins at thousands of RPM while pushing gigabytes of data through a rotating joint. Copper contacts wear out, signals drop, and reliability suffers. Optical slip rings change that equation—but only if you choose a partner who understands the physics and the practical demands. MOFLON, a specialist in high-performance rotary joints, shares hard-won insights on designing optical slip rings that maintain signal integrity at speed. Here’s what separates dependable high-speed rotational connectivity from the rest.
Why Copper Slip Rings Fall Short at Higher Rotational Speeds
As rotational speed climbs, the brush-to-ring interface on a copper slip ring starts to behave less like a stable electrical contact and more like a mechanical fault in waiting. Copper is relatively soft, and the increased surface speed magnifies brush bounce and vibration. Even small imbalances or bearing play translate into intermittent contact, causing arcing and rapid pitting of the ring surface. The debris from this wear then gets trapped between brush and ring, further degrading the connection and accelerating damage.
Heat becomes another compounding factor at higher RPM. The frictional energy at the contact point grows quickly, and copper's oxidation rate rises with temperature. A thin oxide layer forms on the ring, which is far less conductive than pure copper. This layer increases contact resistance, leading to voltage drops and electrical noise that can corrupt sensitive signals. As the ring heats unevenly, thermal expansion can also alter the gap between brush and ring, making the contact force unpredictable.
Beyond wear and heat, high-speed operation introduces dynamic eccentricity and centrifugal forces that copper rings are not well suited to handle. The ring can deform microscopically under its own rotational stress, while brushes may lift off momentarily during each revolution. These micro-interruptions produce electrical transients that are difficult to filter. For applications requiring clean power or data transfer at thousands of RPM, copper slip rings simply cannot maintain the reliable, low-resistance path needed.
Where Rotational Vibration Quietly Kills Signal Integrity
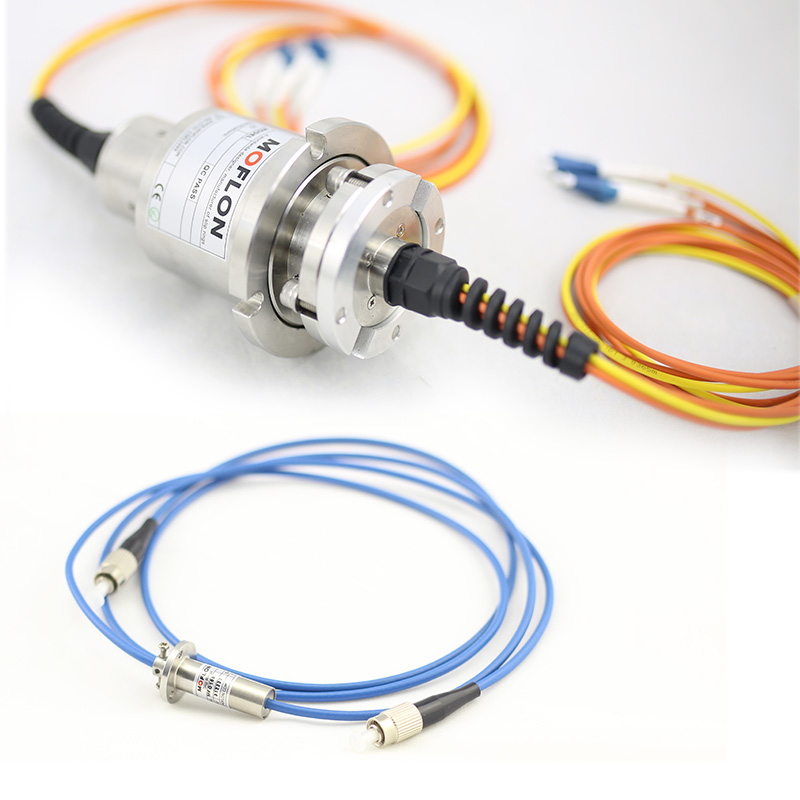
Most diagnostics miss rotational vibration because it doesn't announce itself with dropped packets or full link failure. It works through the clock path: a small periodic mechanical load can pull a crystal or an oscillator just enough to create low-frequency phase modulation. On a high-speed serial eye, that shows up as a slow, rhythmic widening of the crossing point. It looks like power supply noise, but it stays locked to the rotation rate.
The coupling is often indirect. A cooling fan, disk spindle, or even an unbalanced rotor in a nearby pump sends vibration into the board through standoffs and chassis rails. Once that energy reaches a PLL loop filter or a flex cable near a resonant mode, the resulting sidebands sit close to the carrier. Standard compliance tests won't catch it because the board is usually sitting still on a bench, unbolted from the actual rotating assembly.
What makes it hard to debug is that the error signature appears only when the system is assembled and running at normal duty. You can mask it briefly by spreading the clock or tightening the loop bandwidth, but the real fix is mechanical: isolate the oscillator, move the fan off a shared bracket, or shift a mounting hole so the board's first bending mode no longer overlaps the rotation frequency. Until someone straps an accelerometer to the board, the root cause stays invisible.
What High-Speed Testing Reveals About Brush Wear and Tear
Running a brush at elevated speeds exposes failure modes that standard wear tests simply miss. Heat builds up faster than the bristles can shed it, softening the polymer base and accelerating bristle loss. Under a microscope, the tips show signs of melting and the roots develop micro-cracks where the filaments anchor into the backing. These early warnings only surface when the RPM pushes past the manufacturer's comfort zone, which is exactly why high-speed trials matter for anyone pushing tooling to its limit.
Another overlooked factor is aerodynamic flutter. At high rotation speeds, airflow around the brush head tugs at individual bristles, causing them to flex thousands of times per minute. This cyclic loading leads to fatigue fractures deep inside the filament—far from the visible tip wear that most operators expect. Replacing a brush based on outer appearance alone often means discarding units that still have structural integrity, while missing the hidden fatigue that predicts sudden, mid-process failure.
High-speed testing also clarifies the role of debris clearance. Slower operations allow worn particles to drop away naturally, but fast-moving brushes recirculate their own dust, embedding abrasive grit between bristles. This self-inflicted wear pattern accelerates degradation unevenly across the face, creating hot spots that later translate into chatter marks on the workpiece. By mapping these patterns at speed, maintenance teams can adjust cleaning intervals or switch to filament blends that resist re-entrainment, extending brush life without relying on guesswork.
Optical Alignment Strategies That Survive Real-World Shock
Keeping optics aligned after a hard knock is less about brute stiffness and more about letting things move just enough to shed energy without losing position. One approach that works well is pairing a kinematic mount with spring-loaded contacts. The classic three-groove, three-ball arrangement defines the optic's location precisely, but the springs behind each ball allow the assembly to flex under impact and return to the same seat. This avoids the tiny plastic deformations that accumulate when rigid clamps take the full force.
Another practical tactic is to use elastomeric pads or O-rings as the interface between glass and metal. A ring of Viton or silicone with a controlled durometer rating will compress under shock, absorbing high-frequency vibration before it reaches the optic. The trick is to size the pad so it never fully bottoms out; if it does, the metal-to-glass contact becomes a hammer. Machining shallow pockets in the cell to capture the pad also prevents it from extruding sideways under load.
For systems that see repeated impacts, adding a tuned damper to the mounting structure pays off. A small mass on a viscoelastic isolator, placed close to the optic's center of gravity, can draw energy out of the first bending mode. Combined with thread-locking inserts on all fasteners and a torquing sequence that spreads preload evenly, these details make the difference between an instrument that stays on spec after a drop test and one that needs realignment in the field.
Choosing Fiber Types for Duty Cycles Beyond the Datasheet
Standard datasheets rarely tell the whole story when your system runs beyond rated duty cycles. For cyclic loads that push past the published limits, fiber selection becomes less about matching a spec sheet and more about understanding actual stress distribution. Aramid fibers, for instance, handle high tensile spikes well but degrade faster under repeated compression. Glass fibers offer better fatigue resistance in bending, yet their stiffness can transfer too much load to the matrix if the cycle frequency climbs. The trick is to stop asking which fiber is strongest and start asking which one fails gracefully under your specific nonstandard cycle.
When duty cycles exceed datasheet ratings, hybrid fiber architectures often outperform single-material approaches. A thin layer of carbon fiber near the surface can blunt crack initiation from repeated flexing, while a tougher core of ultra-high-molecular-weight polyethylene absorbs shock without adding excessive weight. Another overlooked factor is fiber sizing—the coating applied during manufacturing. Standard sizing is optimized for nominal cycles, but switching to a more ductile sizing can extend service life dramatically once you leave the datasheet envelope. Test coupons with intentionally aggressive cycle counts to see which fiber combination develops microcracks slowly rather than catastrophically.
Don't ignore the matrix either. For duty cycles beyond the datasheet, the resin or thermoplastic often fails before the fiber does. A high-elongation resin paired with a stiffer fiber can create a mismatch that accelerates delamination under repeated thermal cycling. Instead, match the fiber's modulus to the matrix's elongation at break. For high-cycle fatigue at elevated temperatures, consider ceramic or basalt fibers—they offer better dimensional stability and resist creep better than glass, even if their initial tensile strength appears lower on paper. The real specification to watch is not ultimate strength but retained strength after ten thousand nonstandard cycles.
Reworking Existing Rotating Assemblies Without Downtime Nightmares
Reworking a rotating assembly in place sounds like an invitation for a seized bearing or a misaligned coupling, but with the right sequence it rarely turns into a horror show. The trick is to stop thinking of it as a full teardown and start treating it as a controlled surgery: lock out the drive, mark timing positions, and pull only what needs new life. Most crews get into trouble when they yank everything at once, lose the shim stack order, or reuse a gasket that was already weeping. A clean bench, a torque wrench that's actually been calibrated this decade, and a few witness marks with a paint pen will save more time than any fancy tool.
What often bites people is not the mechanical work but the schedule pressure. If you're swapping a worn gear set or re-timing a cam, do it during a planned window, not in the middle of a production spike. Bring in a second set of eyes for the critical measurements—backlash, end play, runout—because a single tired technician can easily misread a dial indicator. And don't forget the soft stuff: update the lubrication plan, check the coupling alignment again after the first heat cycle, and let the machine run unloaded for ten minutes before handing it back to operations. Quiet confidence beats rushing every time.
The real secret to avoiding downtime nightmares is a staged plan that tells everyone what "done" looks like. Write down the expected clearances, torque values, and any rotational direction checks before you start. Keep the old parts until the new ones are proven, and document any variance from the manual. If something feels off—a tight spot every revolution, a new whine under load—shut it down and look again. A rotating assembly that's been reworked properly should feel boringly predictable, not exciting. That's the whole point.
FAQ
Look closely at measured insertion loss and return loss across the full 360-degree rotation, not just static specs. A supplier that provides per-channel test data under vibration and temperature cycling tends to inspire more confidence than one quoting only theoretical limits. Also check how the fiber is managed inside the rotor—tight bend radii can cause micro-cracks that only show up after months of duty.
The core trick is to avoid any moving fiber-to-fiber contact. Many designs use collimating lenses or prisms to bridge a small air gap, which lets the beam pass with minimal disruption as the rotor turns. Because there are no sliding electrical contacts, the bit error rate stays flat and the link remains immune to EMI, even at multi-gigabit speeds.
Wind turbines, medical CT scanners, maritime cranes, and defense turrets are the usual heavy users. In each case, the need to push high-resolution video, radar, or sensor data through a continuously rotating joint makes copper slip rings a bottleneck. Optical paths also remove sparking risks in explosive or fuel-rich environments.
Sealing and thermal stability often separate the two. A robust unit will use precision bearings, a dry nitrogen purge or IP-rated enclosure, and materials that don't shift focal length as temperature swings. Marginal designs may perform well on a bench but drift out of alignment after thermal expansion or bearing wear, causing intermittent dropouts.
Because active electronics add heat, power draw, and failure points inside a rotating joint that is hard to access. A passive lens- or prism-based optical path needs no amplification as long as the link budget supports the modest losses, typically under 2 dB per channel. That simplicity translates to longer service intervals and fewer field returns.
It lets a single rotating joint carry both high-bandwidth optical channels and lower-speed power or control signals. Engineers can then design a turret or crane with one pass-through instead of stacking separate rings, saving axial space and simplifying cable routing. The trick is shielding the electrical section well enough so it doesn't couple noise into the optical receivers.
Ask for accelerated life test data that includes continuous rotation at rated speed, thermal cycling between operational extremes, and periodic loss measurements over millions of revolutions. A credible vendor will also offer a short in-situ burn-in period with real payload traffic. Those steps catch alignment drift and connector seating issues that would otherwise surface after installation.
Each additional fiber channel forces tighter optical alignment tolerances and increases crosstalk risk if the beam paths are not physically isolated. As the rotor diameter grows to accommodate more collimators, bearing runout and frame flex can degrade coupling efficiency. Good designs mitigate this with modular optical cartridges that can be replaced without realigning the whole assembly.
Conclusion
Copper slip rings have long been the default for rotating electrical connections, but their limits become obvious once rotational speeds climb. Contact brushes generate friction heat, produce debris, and develop hot spots that degrade conductivity; at higher RPMs those failure modes accelerate until intermittent dropouts turn into hard faults. High-speed testing doesn't just reveal faster brush wear—it exposes how abrasive particles migrate into bearing surfaces and contaminate nearby electronics. Even before outright failure, rotational vibration quietly undermines signal integrity by causing micro-scale contact bounce. That bounce translates into bit errors, jitter, and lost packets on data lines, often without triggering alarms. Replacing contact rings with optical fibers removes the wear mechanism entirely, but only if alignment survives real-world shock.
Robust optical alignment for rotating assemblies demands more than bench-level precision; it needs tolerance for mounting flex, thermal expansion, and shock loads from the surrounding machine. Some designs use lensed fiber collimators with spring-loaded retention, while others rely on passive alignment features that maintain beam pointing under vibration. Fiber selection matters just as much: standard single-mode patch cords are rated for static installations, not millions of flex cycles or sustained rotation at elevated temperature. Specialty fibers with high fatigue resistance and coated buffers outlast datasheet predictions by wide margins. Finally, retrofitting existing copper-based assemblies need not trigger a full teardown. Modular optical cartridges, drop-in rotary joints, and staged cutover plans let teams swap channels during scheduled windows—turning a risky overhaul into a controlled, low-drama migration.
Contact Us
Contact Person: Xiangpin Li
Email: [email protected]
Tel/WhatsApp: 86 186 1706 8578
Website: https://www.moflon.com