Portable Ozone Machine Factory Quality and Production Insights
2026-09-17
A portable ozone machine can look flawless on the outside and still carry hidden compromises inside. Factory quality isn't a marketing claim; it's a chain of decisions about seals, plates, and test cycles that most buyers never see. LUFUTATECH opens up that hidden layer, sharing production insights that reveal why some units run quietly for years while others degrade after a few months. The clues are in the manufacturing details.
Inside the Assembly Line Where Portability Meets Ozone Output
Walk the floor of any modern ozone generator plant and you will quickly notice that the assembly line is not a single, linear path but a choreographed tension between two competing demands: compact, carry-friendly design and raw ozone output. Every station reflects a deliberate trade-off. On one side, technicians nest ceramic plates and solid-state power supplies into housings barely larger than a lunchbox, shaving grams with milled aluminum corners and snap-fit seals. On the other side, quality checks push those same units to crank out high-concentration ozone streams that would overwhelm a fixed industrial unit a decade ago. The result is a product that feels light in your hand yet meters out ozone levels once reserved for bulky, stationary systems.
What makes this balance possible is less about one breakthrough component and more about how the line sequences its verification steps. After the corona cell is mounted, workers run a brief high-voltage stress test that intentionally exceeds normal operating voltage for ninety seconds. This catches micro-cracks in the dielectric coating that would otherwise pass a visual inspection. Then, instead of a separate station for portability checks, the same assembly cell includes a drop-test fixture and a weight-scale audit—so a unit cannot leave the station with both a stellar ozone concentration reading and an overweight, fragile shell. The line supervisor calls this “forcing the conflict,” because if a design fails either axis, it loops back to rework rather than moving forward with a silent compromise.
The final stretch of the line is where the two priorities visibly meet. A technician holds a fully assembled unit in one hand while clamping its output port to a calibrated ozone analyzer. The readout climbs into the parts-per-million range that customers expect for odor remediation or water treatment, and yet the unit barely warms the technician’s palm. Next to the analyzer sits a luggage-scale-style hook where the unit’s total weight is logged against the day’s target. Units that pass both gates get a matte finish serial plate and a foam-lined box no larger than a hardcover novel. It is a strange sight: high-output ozone hardware treated like a consumer gadget, but that is exactly the point of this assembly line—portability does not dilute potency; it disciplines it.
Why Ceramic Plates and Sealed Chambers Decide Longevity
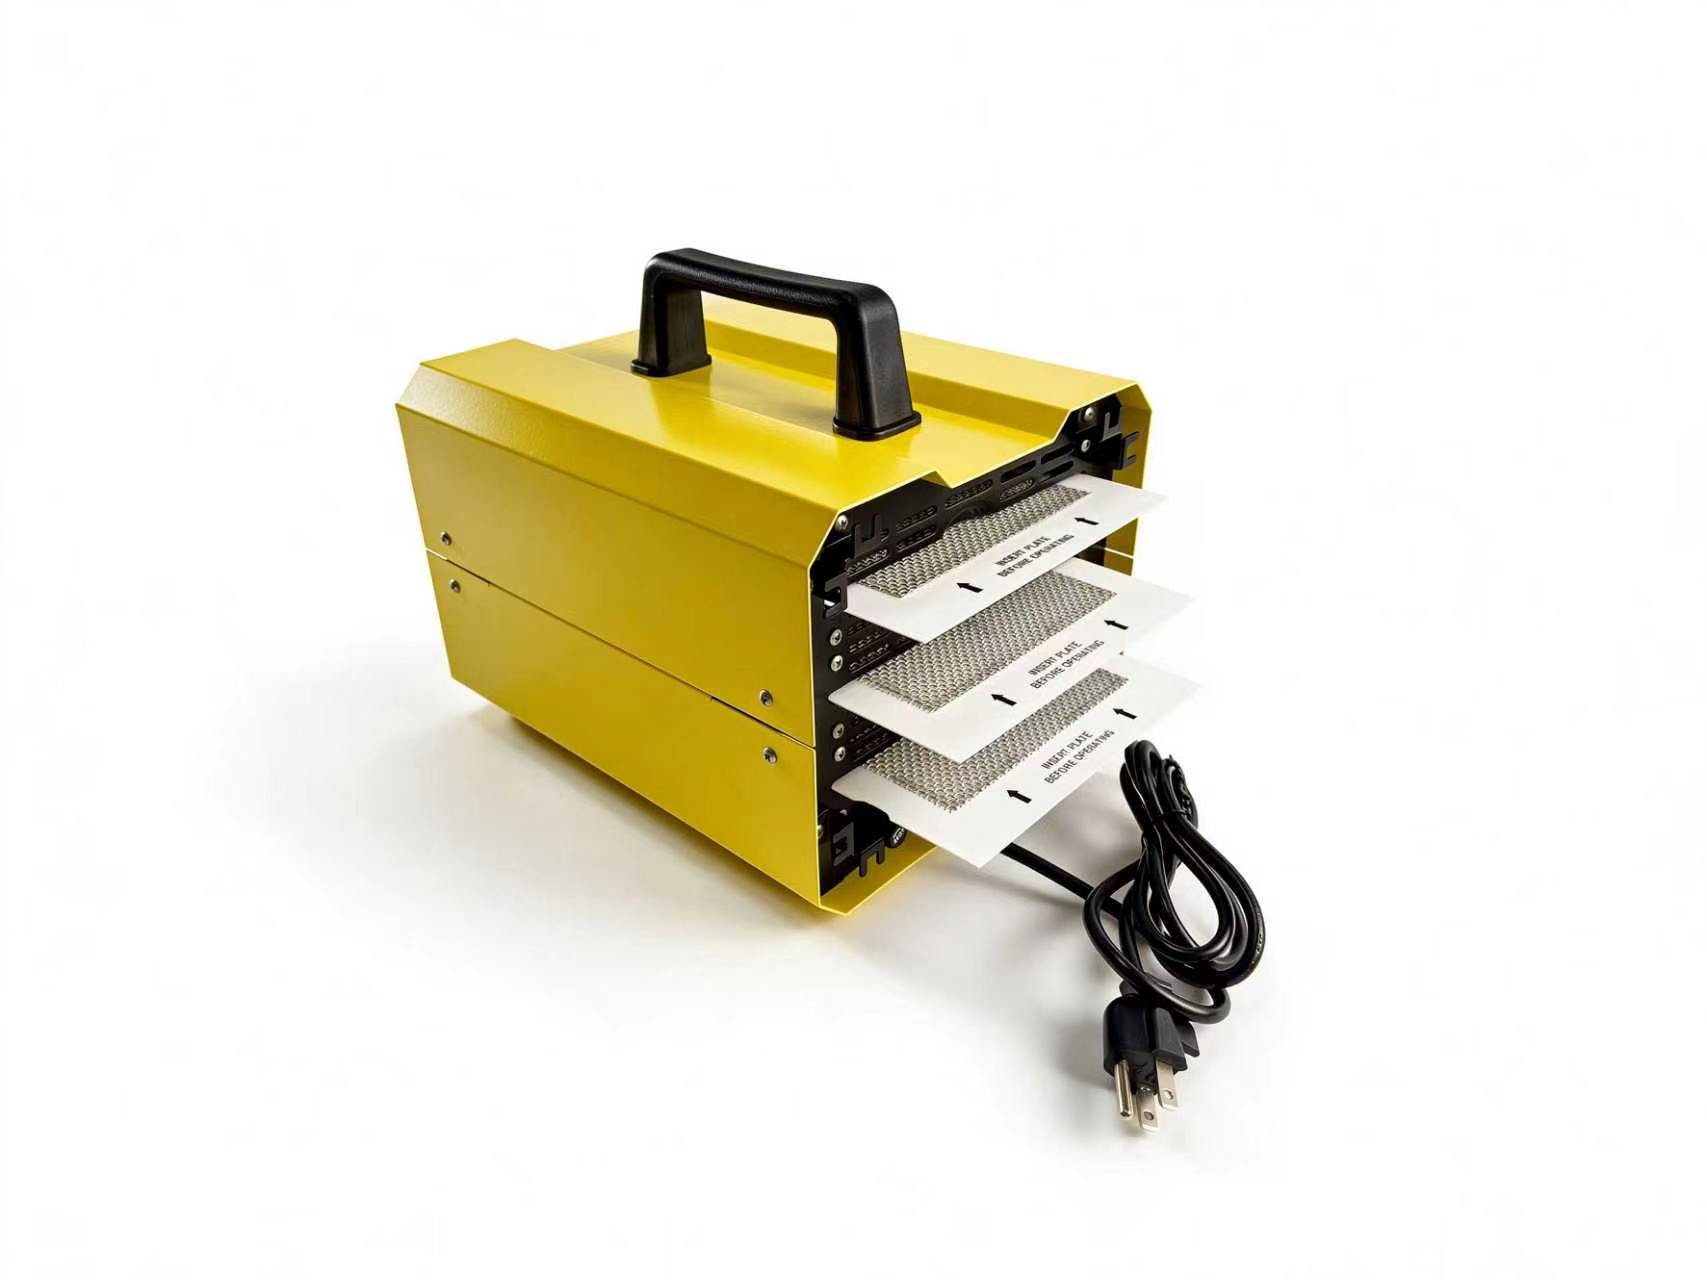
Ceramic plates earn their reputation because they spread heat in a way that feels seamless but also protects the hardware underneath. When a plate has hot spots, the surrounding material works harder to compensate, and that uneven stress quietly shortens the component's life. A high-quality ceramic surface also shrugs off buildup from styling products and daily wear, so the heating layer stays intact instead of slowly degrading with every pass.
Sealed chambers play a quieter role, but they're just as decisive. Moisture from bathrooms, residue from sprays, and fine dust all try to creep into the internal wiring and heating elements. Once inside, they accelerate corrosion and can cause sudden failure long before the device should retire. A properly sealed chamber keeps those particles out, preventing the slow internal damage that no amount of external cleaning can fix. Together, ceramic plates and tight seals remove the two biggest threats to durability: uneven thermal stress and environmental contamination.
From Raw Polymer Pellets to a Finished Portable Unit
The process starts with raw polymer pellets, often a tailored mix of polypropylene, impact modifiers, and UV stabilizers, dried to remove absorbed moisture before entering the hopper. Under controlled heat and shear inside the barrel, the pellets melt into a homogeneous flow and are injected or extruded into steel molds that form the outer shell, internal frame, and mounting bosses. Cooling lines then pull heat away quickly, locking in dimensions and reducing warpage before the parts are ejected.
After ejection, parts go through trimming, deflashing, and sometimes ultrasonic welding to create durable, dust-resistant seams. Threaded brass inserts are heat-staked into boss locations, and exterior surfaces receive a light texture for grip and scratch resistance. Each piece is measured with simple go/no-go fixtures to catch shrinkage or sink marks before assembly.
On the assembly bench, the molded housing halves are mated with the battery, circuit board, and small hardware like gaskets and screws. A short functional test checks power draw, button response, and seal integrity, followed by a drop test on a corner of the unit. Units that pass are wiped down, labeled, and packed into retail boxes for shipping.
The Quiet Standards Behind Consistent Ozone Concentration
Ozone levels rarely drift by accident. Behind the steady numbers on monitoring dashboards, a set of quiet standards works like an invisible scaffold. These are not headline-grabbing rules, but rather deeply embedded calibration protocols, reference methods, and cross-check routines that labs and stations quietly follow. They define how air is sampled, how instruments are zeroed and spanned, and how data gets flagged when something drifts out of tolerance. Without them, the same ozone molecule could be measured a dozen ways depending on who is holding the sensor.
What makes these standards effective is their stubborn insistence on repeatability. A photometer is not simply turned on in the morning; it undergoes a documented warm-up, a known gas mixture challenge, and a comparison against a transfer standard that traces back to a national reference. These steps are not glamorous, but they keep a station in Tucson from disagreeing with one in Berlin. The quiet part is intentional: when everything aligns, nobody notices. That is exactly the point.
Over time, the standards also absorb small lessons. A tubing material that off-gassed unexpectedly, a pressure correction applied too late, a zero drift that appeared only on humid afternoons — each becomes a note in the next revision of the protocol. The result is a living document that grows more robust without fanfare, quietly holding the line so that a reported ozone concentration of 70 parts per billion means the same thing to a regulator in Osaka and a researcher in Reykjavik.
How Small-Batch Testing Catches What Mass Production Misses
A production line hums along, turning out thousands of identical parts, and that steady rhythm can hide small problems until they turn into expensive recalls. Small-batch testing breaks that rhythm on purpose. By running a limited number of units through the same tooling and processes that will be used at full scale, you see how materials actually behave under real conditions—not just how they should behave in a simulation. A slight warping in a bracket, a cure time that drifts with humidity, a seal that fits fine at room temperature but leaks after thermal cycling: these are the details that only surface when someone is watching a short, careful run.
Mass production rewards consistency, but it often assumes the first few units were representative. Small-batch runs challenge that assumption. When you build fifty units instead of fifty thousand, you can afford to measure every one, cut a few open, and push the rest until they fail. That kind of destructive inspection is impractical at full volume, yet it reveals weak points that statistical sampling alone will miss. A bad batch of adhesive, a shift in supplier tolerances, or a tool wearing out sooner than expected shows up as a pattern in the data from that small run—not as a mystery to be investigated after customers start complaining.
There is also a human factor. Engineers and operators pay closer attention when they know the run is small and the goal is learning, not output. They ask questions they would skip if the line were moving at full speed. That curiosity turns into design tweaks, better test fixtures, and clearer assembly instructions before the expensive tooling gets locked in. The result is a product that has already met reality once, on purpose, before it has to survive mass production by accident.
What Factory Floor Data Reveals About Real-World Durability
Assembly line sensors capture far more than cycle counts. They record the exact torque loads, vibration signatures, and thermal swings a component endures hour after hour. When engineers dig into that stream, they stop guessing about which parts will fail first—they see it in the data. A bearing that lasts 10,000 hours on a clean test bench might degrade twice as fast when exposed to the fine metal dust and irregular shocks common on a busy factory floor.
What sets this apart from traditional durability testing is the messiness. Lab conditions are controlled; real production environments are chaotic. Voltage spikes, unplanned stops, operator overrides, and uneven material batches all leave traces in the telemetry. By correlating those events with later failures, maintenance teams can move away from fixed replacement schedules and toward condition-based interventions. One automotive supplier, for instance, found that 80% of unexpected downtime came from just three failure modes—all of which were invisible in accelerated life tests but plain as day in six months of floor data.
The payoff isn't only fewer breakdowns. It's a tighter feedback loop between design and operation. When durability claims are grounded in actual usage patterns rather than idealized duty cycles, product engineers can reinforce the right weak points without overbuilding the rest. That means lighter components, lower material costs, and machines that hold up where it actually matters.
FAQ
Each unit goes through a high-voltage arc test first, then we run it for 15 minutes and measure ozone concentration with a calibrated sensor. After that we check fan speed, button response, and any unusual vibration. A random sample from every batch gets a 24-hour continuous burn-in to catch early failures.
We calibrate the ceramic ozone plates or quartz tubes against a reference gas sensor before assembly. Each batch records the voltage-current curve and adjusts the driver frequency slightly to match the same output range. It’s not a set-and-forget process; temperature and humidity in the workshop can shift readings, so we retest every morning.
The internal electrode should be stainless steel or gold-plated, not bare copper. For the housing, ABS or PC/ABS alloy holds up far better than cheap polystyrene because ozone slowly degrades brittle plastics. Silicone tubing and nickel-plated connectors also prevent cracking and poor contact after a few months of use.
The big ones are high-voltage arcing from poorly insulated wires, early ozone plate decay from moisture, and fan failure from dust buildup. We tackle those by potting the transformer, adding a small desiccant pack inside the housing, and using sealed ball-bearing fans with an intake filter. Button sticking is another sneaky issue, so we do a tactile and cycle test on every unit.
If it’s a standard model with your logo and different packaging, 7 to 15 days is realistic. If you need a new housing shape, custom PCB layout, or a novel control panel, expect 30 to 45 days including mold and tooling. Adding a specific plug standard or changing the power adapter can add a week depending on component lead times.
At minimum, CE and RoHS for most markets, plus FCC if there’s any wireless or digital control. If the unit ships with an external power adapter, you’ll likely need UL, ETL, or GS depending on the country. For anything marketed with health or medical claims, the factory should have experience with FDA 510(k) or CE medical documentation, otherwise it’s a red flag.
Yes, and that’s where a lot of low-cost units fall short. We add a one-button timer that shuts off automatically, an optional motion sensor so it won’t run when people or pets are present, and a gasket-sealed chamber with a pressure test to confirm no gas escapes around the seams. Some clients also want a low-concentration mode for small spaces, which we tune by lowering the drive current rather than just covering the outlet.
It’s mainly about the fan and airflow path. We use a low-noise fan with an optimized blade angle and place it away from the ozone plate so it doesn’t whistle. Adding a small muffler or acoustic foam inside the outlet duct cuts maybe 3 to 5 dB without restricting airflow. Then we sweep the driver frequency to avoid a resonance that makes the whole shell vibrate at certain output levels.
Conclusion
Inside a portable ozone machine factory, the assembly line is where portability has to meet consistent ozone output without compromising either. Workers fit ceramic plates into compact housings, and those plates, paired with properly sealed chambers, determine whether a unit lasts months or years. The journey from raw polymer pellets to a finished handheld device is more than just molding shells; every snap-fit, gasket, and weld point gets checked because a tiny leak can silently drop ozone concentration below spec. The quiet standards here aren't written on posters but built into torque settings, seal compression tests, and plate alignment jigs.
Small-batch testing remains the unsung hero of production. While mass production runs at speed, pre-production lots are deliberately stressed—cycled on and off, run in humid conditions, left vibrating on benches—to catch failures that only show up after weeks of real-world use. Factory floor data from returned units and endurance benches feeds back into ceramic plate thickness, chamber geometry, and even polymer grade choices. The result is a portable ozone machine that doesn't just pass a single QC check but holds its output and structural integrity across hundreds of hours, which is exactly what buyers in field service, hospitality, and residential settings actually need.
Contact Us
Contact Person: Paul Luo
Email: [email protected]
Tel/WhatsApp: 0086-19966314501
Website: https://www.lufutatech.com