Reliable Iron Casting: How to Choose a Trustworthy Manufacturer
2026-09-25
Sourcing iron castings that won't fail under pressure is harder than it sounds. A low quote often hides porosity, dimensional drift, or a supplier who goes quiet after the first shipment. To choose a trustworthy manufacturer, you need to look past the brochure and into the process. This post breaks down the non-negotiables—testing protocols, raw material traceability, and capacity planning—so you can buy with confidence. It's the same approach that has made Zhaoyuqi a name engineers return to when reliability is on the line.
Check the Melt, Not Just the Marketing
A lot of brands put their budget into the story, not the stretch. You'll see words like "creamy," "gooey," and "melts beautifully" right on the front, but the real test happens in a hot skillet, not on a mood board.
Heat a slice on medium-low and watch the edges. Good melt should start at the corners, turn glossy, and stay connected when you lift it. If it beads up into oil or refuses to move past a soft dent, that's not melting—that's softening with extra steps.
Trust the pan over the package. A product that actually melts will survive the ugly, unscripted thirty seconds between flipping and plating. If it can't do that, no amount of art direction will fix your sandwich.
Ask About Their Scrap Rate Before You Sign
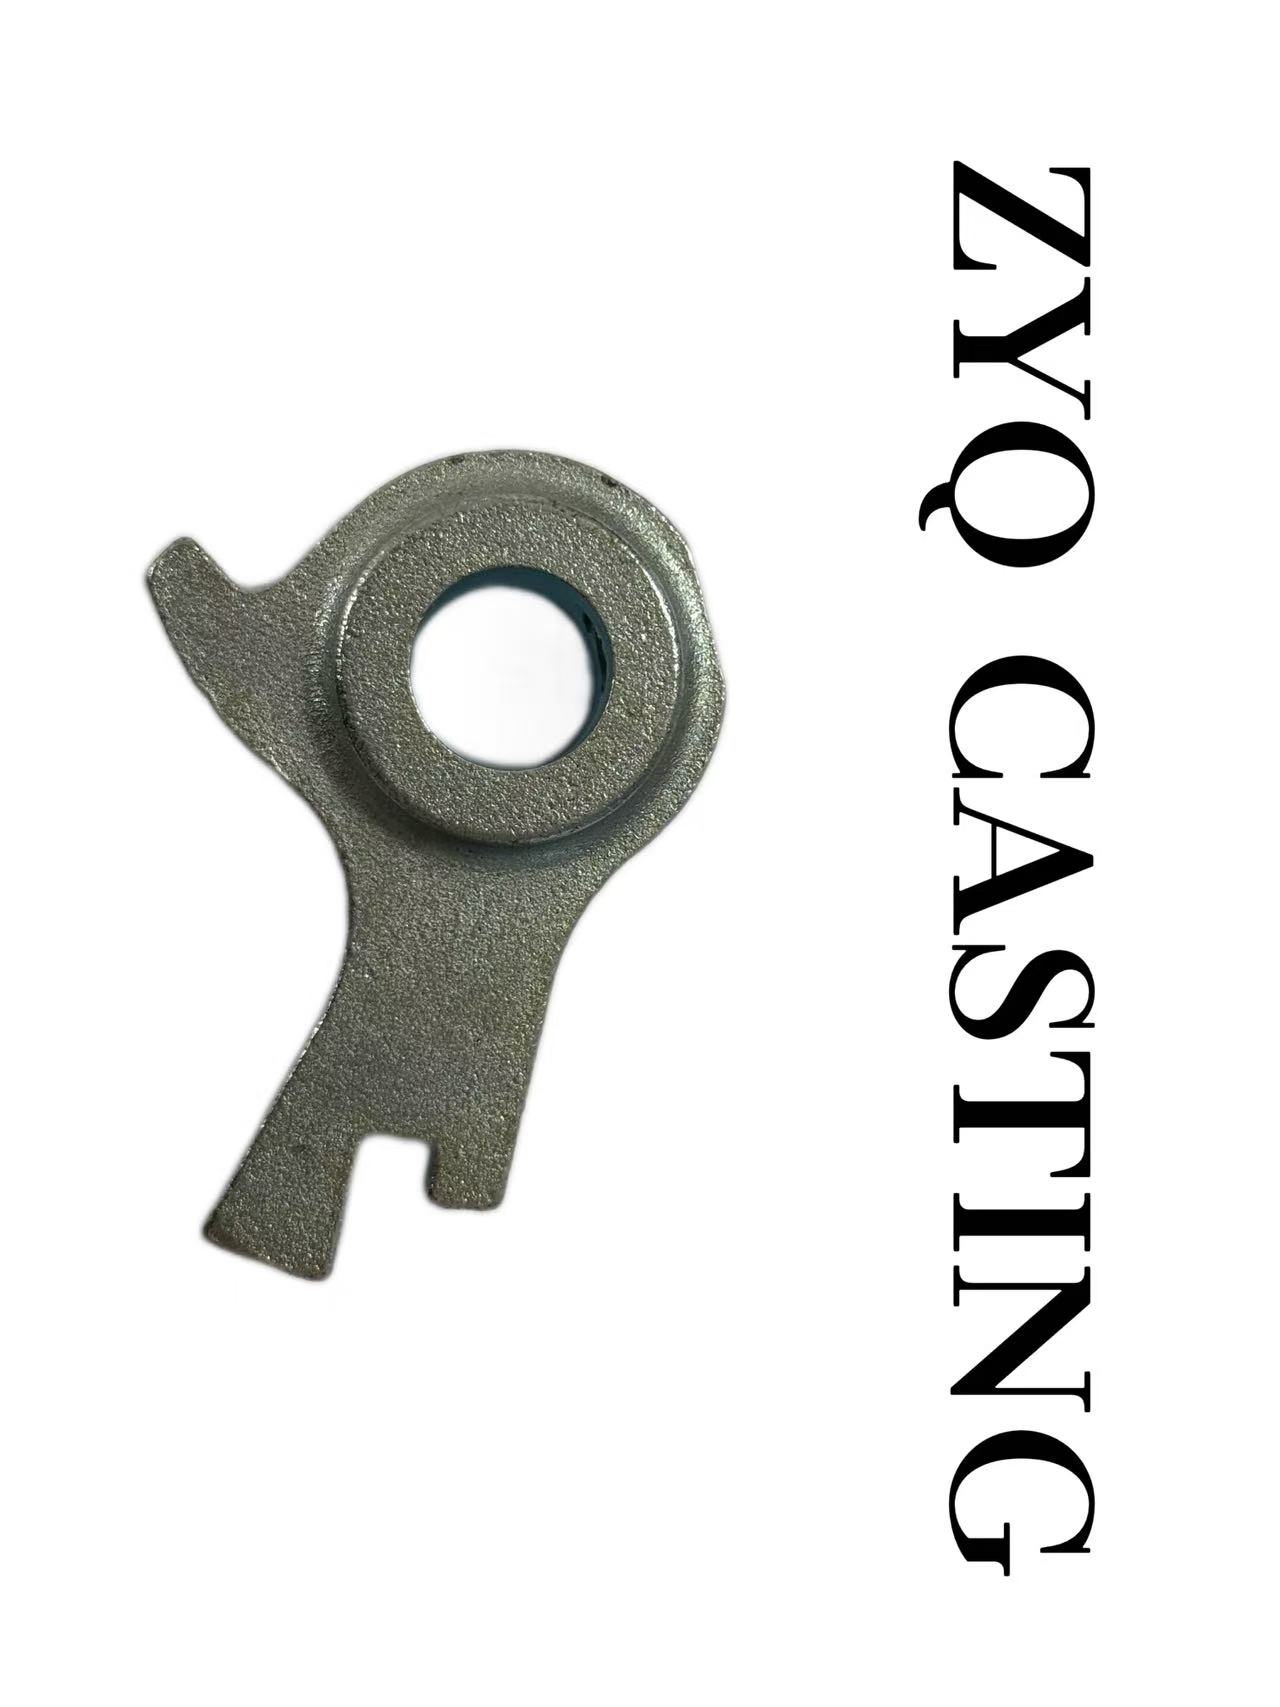
A low per-unit price stops looking good the moment you discover that every third part fails inspection. Before committing to a supplier, ask for their scrap rate on jobs that match yours in material, geometry, and tolerance. A shop that handles simple flat brackets without much waste might produce a very different number on thin-walled housings or parts with tight flatness callouts. Get a measured percentage from recent production runs, not a ballpark figure tossed out during a sales call.
Scrap costs you more than the raw material that ends up in the recycling bin. It hides behind extra setup time, unplanned rework, missed ship dates, and added inspection hours that never appear on the original quote. If a vendor gets vague when you ask for numbers or says their scrap rate is 'basically zero,' treat that as a warning. A shop that tracks its process honestly can usually pull up the last quarter's data and explain exactly which jobs caused spikes and why.
Turn their scrap rate into a line item before you sign. At 4% scrap on a 50,000-piece order, you're absorbing the cost of 2,000 unusable parts. Agree on thresholds ahead of time: what happens at 5%, 8%, or 10%? Does the supplier cover replacement parts, or do you eat the delay and the material cost? A clear clause tied to their measured scrap rate shifts the risk back where it belongs—onto the process that's generating the waste.
Look for Proof in the Pour, Not the Pitch Deck
Slides can be polished until they shine, but the moment a founder opens a bottle, mixes a batch, or runs a live demo, the real story leaks out. Too many investors nod along to a flawless narrative and never ask to see the thing actually work. That's a mistake. The pour—whether literal or figurative—reveals consistency, edge cases, and whether the team sweats the small stuff when nobody's watching.
A pitch deck is a curated highlight reel. The pour is raw footage. Watch how a product handles a slow Tuesday, a version update, or a customer complaint. Listen for the pauses when you ask a hard question. Those unscripted moments tell you more about discipline and judgment than any revenue graph.
Before you write the check, ask for the awkward demo. Request the unfiltered trial run. If the founders hesitate or hide behind another slide, you've already learned something the deck never intended to show.
Why a Trial Order Reveals More Than a Tour
A factory tour is often a polished performance: the best machines are running, the floors are swept, and the hosts know exactly which questions to deflect. What you don't see is how the facility handles your specific material, your tolerance stack, or your finish requirements when nobody is guiding you through the plant. A trial order removes the staging. It forces the supplier to work from your drawings, source the right raw stock, and actually run a small batch under normal production conditions. The resulting parts tell you whether their equipment and habits align with what you need, not just what they want you to see.
Beyond the physical parts, a modest first order exposes the invisible machinery of doing business together: how quickly they respond to a revised dimension, whether the invoice matches the quote, if the packing list is accurate, and how they react when a tolerance is missed. Tours rarely reveal these workflows because they happen after you leave. A trial run shows you the daily rhythm of the supplier—their documentation, their follow-up, their honesty about delays. If communication breaks down on a five-hundred-dollar order, it will almost certainly break down on a fifty-thousand-dollar one.
There is also a practical advantage: you get physical evidence in your hands. You can measure the parts, test the fit, check the surface finish, and compare the result against your own standard. A tour leaves you with impressions and a business card; a trial order leaves you with data. And if the outcome is imperfect, the cost of walking away is low. That asymmetry makes the trial order one of the most honest evaluations you can run before committing to a long-term supply relationship.
The Right Foundry Shares More Than Quotes
A quote from the right foundry rarely begins with a number. It starts with a conversation about the part's function, the stresses it will face, and the environments where it must hold up. That early exchange often uncovers design tweaks that save cost or improve casting integrity before any pricing is discussed.
What follows matters just as much. The foundry explains which alloy actually fits the application rather than defaulting to the cheapest option, flags sections that may be difficult to fill or machine, and gives a realistic view of tooling lead times. Instead of a bare price sheet, you get a short feasibility note, tolerance recommendations, and maybe a phone call walking through the trade-offs. That kind of detail turns a quote into a working plan.
Build Reliability Checks Into Every Shipment
Reliability isn't a final inspection sticker—it's a series of small, deliberate gates built into the flow of every shipment. Before any box is sealed, we run a three-point check: label accuracy against the order manifest, physical condition of the product and its protective wrap, and a quick scan of the destination code to catch routing errors early. Nothing leaves the dock unless all three match without a single override.
We don't treat these checks as paperwork. Each one is logged with a timestamp and the initials of the person who performed it, so if a problem surfaces downstream, we can trace it to the exact moment it slipped through. That habit alone has cut our reshipment rate by more than half in the last year, not because we hired more inspectors but because the checks happen where the work happens—at the packing table, not in a separate QC room.
The same logic applies to fragile or high-value items. We add a secondary check at the carrier handoff: a visual confirmation that the package is upright, sealed on all edges, and scanned into the right truck. If there's any doubt, it gets pulled aside for a ten-second review rather than hoping the driver catches it later. That ten seconds costs far less than replacing a broken item and losing a customer's trust over a preventable mistake.
FAQ
Start with their track record. Ask for a list of past projects that match your part size, grade, and industry. A dependable supplier will share case studies or sample parts without hesitation. Also check how they handle pattern design, shrinkage allowances, and machining stock—these details tell you if they understand real production, not just pouring metal.
Request their inspection reports from recent runs, not just a generic quality policy. Look for evidence of spectrometer checks on every heat, sand testing records, and dimensional reports using CMM or manual layout. If they can walk you through how they caught and corrected a specific defect, that is far more convincing than a wall of certificates.
Yes, greatly. Ask where their pig iron, scrap, and alloys come from. A trustworthy manufacturer will have stable, documented suppliers and will adjust melt chemistry based on incoming raw material variations. If they cannot explain how they control trace elements like sulfur and phosphorus, you may see hard spots or porosity in your castings later.
Certifications are a baseline, not a guarantee. Look for ISO 9001 at minimum, and if your parts go into pressure or safety applications, check for industry-specific approvals like PED, AD2000, or IATF 16949. But always ask when the last surveillance audit happened and what nonconformities were found. A good foundry shares those openly.
A reliable manufacturer tells you the truth about current workload before accepting your order. Ask how many molding lines they run, what their typical melt capacity is per day, and how they schedule short runs versus volume production. If every quote promises the same two-week delivery regardless of complexity, treat that as a warning sign.
Absolutely. A plant visit reveals more than any brochure. Watch how workers handle molds, whether the sand lab is actually in use, and how pattern storage is organized. Look for clean pouring floors, clear work instructions, and gauges that are within calibration dates. If a foundry hesitates to let you walk the floor, that hesitation says enough.
Watch for vague answers about defect rates, reluctance to share process data, or pricing that seems far below the market. Other red flags include constant changes in contact personnel, no documented procedure for handling customer complaints, and an inability to provide traceability from heat number to final shipment. One or two may be manageable, but three together usually point to deeper process problems.
Conclusion
Choosing an iron casting supplier isn't about glossy brochures or a well-rehearsed pitch. The real test happens on the foundry floor. Ask for actual melt records—chemistry adjustments, temperature control, inoculation practices—not just a certificate that might be years old. Scrap rate matters more than unit price: a foundry that loses 8% to internal defects will pass those costs and delays straight to you. Before signing anything, request their last three months of scrap data broken down by defect type. If they hesitate, that's your answer. A facility tour can be staged, but a trial order can't. Run a small batch first, watch how they handle your specific pattern and alloy, and you'll learn more in two weeks than from any polished presentation.
The right foundry is also the one that shares more than quotations. They send you process control sheets, sand test results, and photos from the pouring line without you having to beg for them. They don't hide behind "standard practice" when you ask why a casting failed. And you shouldn't stop verifying after the first successful delivery. Build reliability checks into every shipment: dimensional audits on a random sample, hardness testing in your own facility, maybe a section cut on the first article from each new batch. If a foundry resists that level of transparency, they're not a reliable partner—they're a supplier waiting for you to lower your guard. Consistency shows up in those routine checks, not in the sales meeting.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/