Top Press Brake Manufacturing: How to Identify Industry Leaders in Precision Bending
2026-11-02
Precision isn’t a buzzword in press brake manufacturing—it’s the entire game. Yet with countless suppliers promising tight tolerances, distinguishing true industry leaders from the rest takes more than a spec sheet. Whether you’re upgrading a job shop or running high-mix production, the wrong choice reveals itself in every imperfect bend. In this guide, we’ll unpack the signals that actually matter: build quality, control responsiveness, after-sales support, and the engineering mindset behind the machine. And if you’ve been paying attention, you’ve likely noticed JIAN MENG emerging as a name worth knowing in precision bending.
Beyond the Spec Sheet: Testing Real-World Bend Accuracy
Every press brake ships with a spec sheet full of numbers, but those figures are measured under ideal lab conditions. Real metal has springback, grain direction, and thickness variation. That's why we test bend accuracy on actual production stock rather than relying on factory charts. You'll notice the difference when a 90-degree bend holds its angle on the first shot, not after a series of trial bends and corrections.
One common blind spot is how tooling wear shifts results over time. A die that starts out precise can drift by half a degree after a few thousand cycles, especially with high-strength steel. Our testing protocol includes periodic sample bends throughout a run, checking angles with a digital protractor and adjusting the ram position on the fly. That's not something you'll find in a brochure, but it's what keeps your parts within tolerance when the material isn't perfectly uniform.
Another factor is machine deflection under load. The center of a long bed may flex slightly, causing the bend angle to vary from the ends. Spec sheets rarely mention this, but real-world testing reveals it. By measuring a full-width bend and comparing left, center, and right angles, we can compensate with crowning adjustments. This hands-on approach means fewer rejected parts and less time spent fighting the machine.
The Support Story: What Happens After Installation
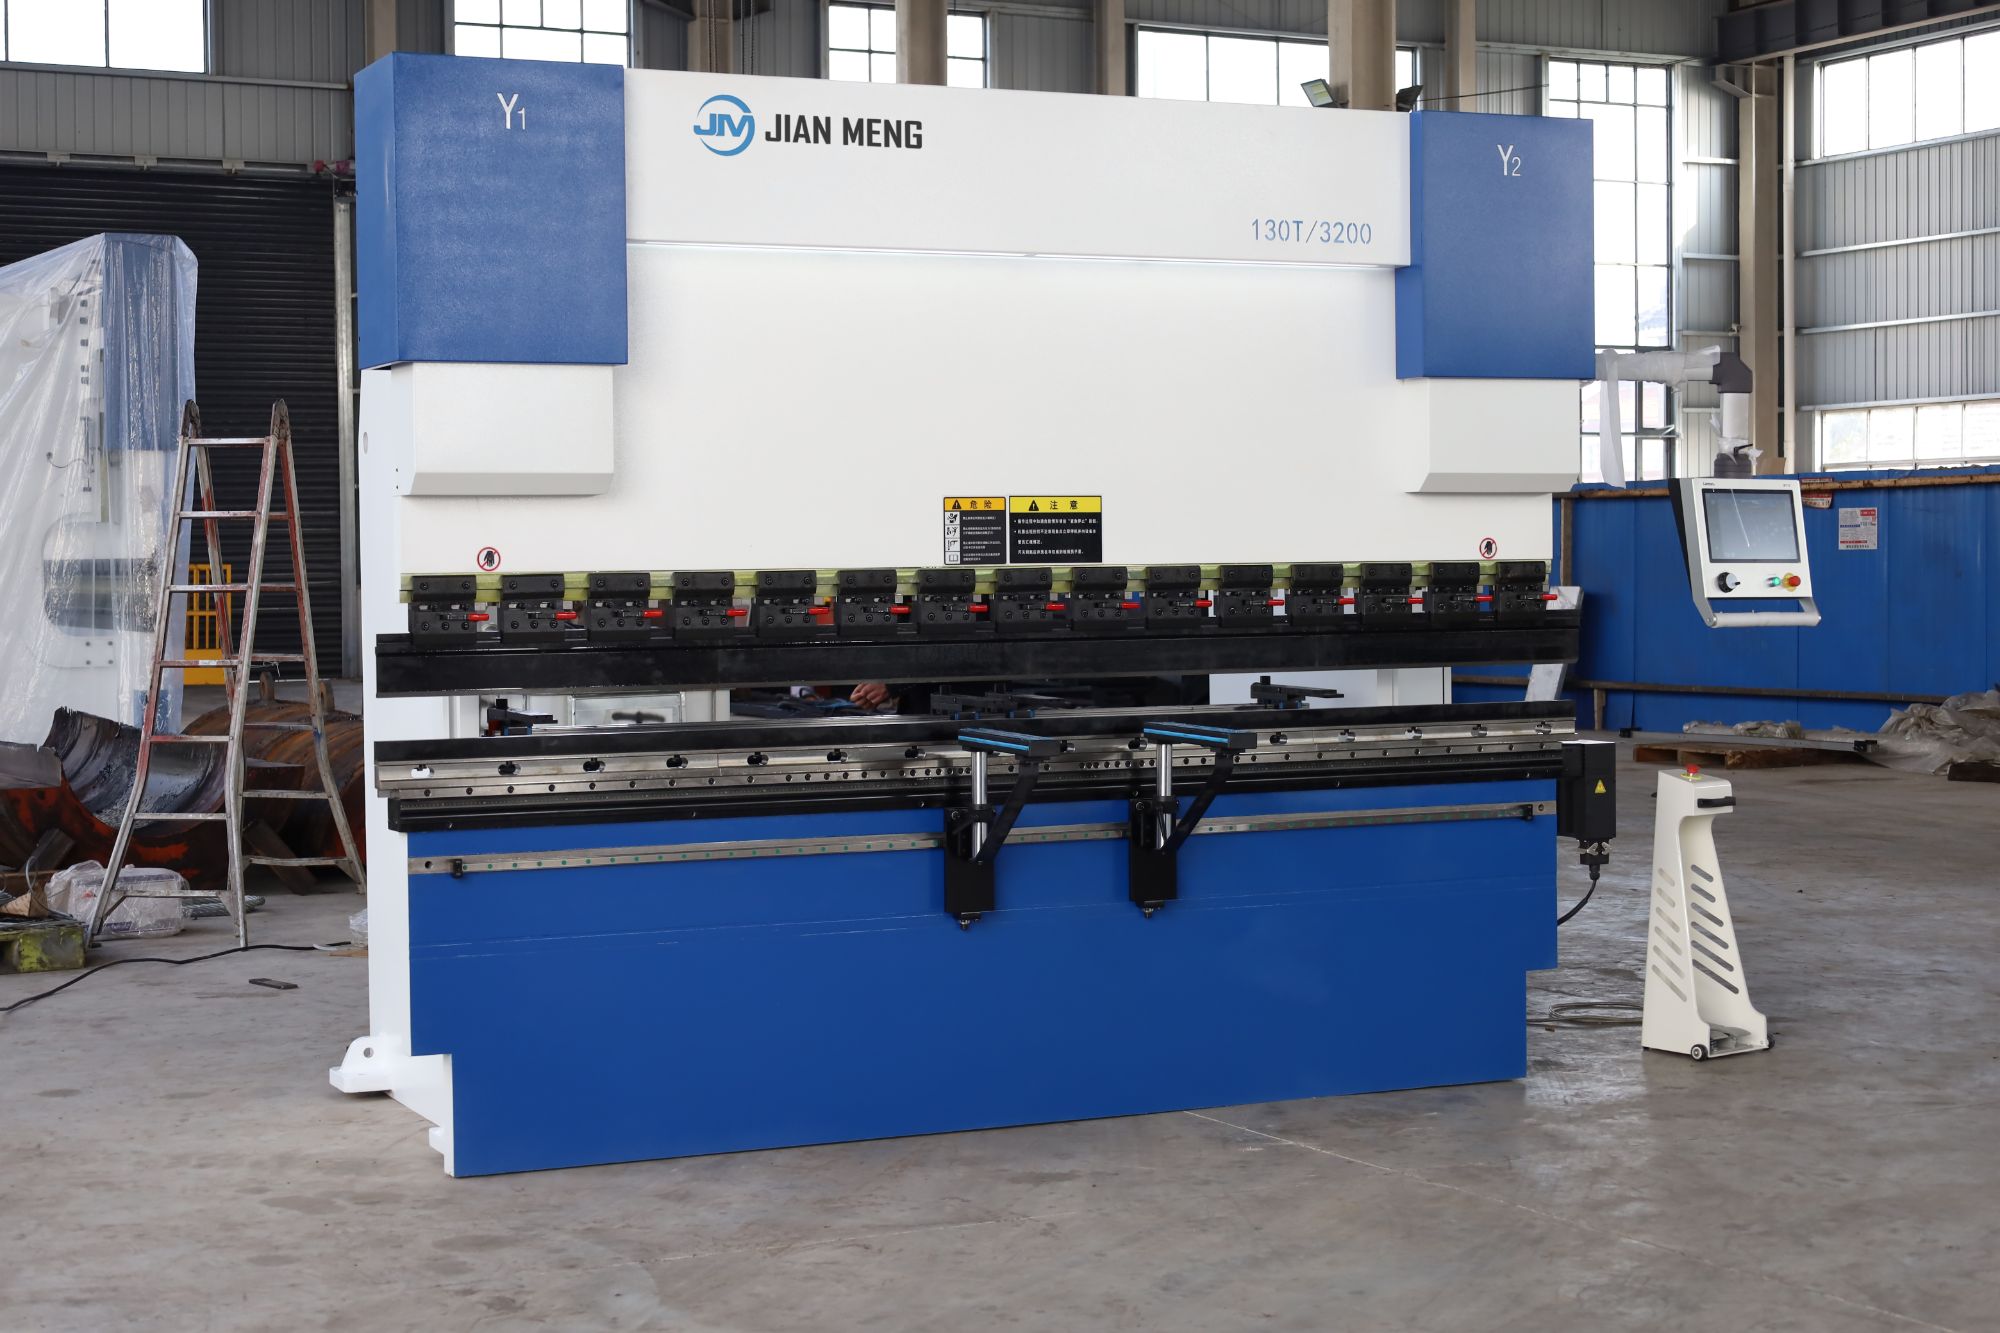
Once the install is finished, the support story keeps going. A member of the team reaches out within a day to make sure everything is behaving the way you expected. It's a quick, human check-in rather than an automated blast, so if something feels off during those first few hours, you can say so directly.
We also set up a follow-up conversation a couple of weeks later. By then, you've had time to use the system in real conditions, and small friction points start to show. That call is for walking through adjustments, answering the questions that only come up after daily use, and tightening anything that needs it.
After that, the channel stays open without layers of phone trees or ticket forms. You'll know who to contact, and we keep notes on your setup so you're never repeating the same background details from scratch.
Custom Tooling and Adaptive Engineering in Practice
Most production shops carry a drawer full of jigs that solve yesterday’s problems. The real difference shows up when a part arrives with an awkward overhang, a tight bore, or a tolerance that makes standard clamps useless. Custom tooling starts there—not with a CAD library, but with the machinist measuring the actual stock, checking runout by hand, and sketching a fixture that holds the part without fighting the setup. In one case, a batch of thin-walled aluminum housings kept deforming under conventional jaws. A set of machined soft jaws with a split ring support and a torque-limited clamp brought scrap down from eleven percent to under two.
Adaptive engineering in this context means changing the process instead of forcing the print. When a standard end mill chattered across a deep pocket, the fix wasn’t a slower feed rate; it was regrinding the tool with a shorter flute length and adding a spring pass at a different radial engagement. Small shops often do this quietly—adjusting tool geometry, remounting a part on a sine plate, or building a dedicated subplate overnight. These choices rarely make it into a formal workflow, but they accumulate into a shop’s ability to take on work that larger vendors reject as unprofitable.
The practice lives in the details of each repeat job. A fixture that started as a one-off for a prototype often gets revised after the first run: a locating pin moved half a millimeter, a clamp repositioned to clear a probe path, a stop added to keep the operator from loading the part backward. Those revisions are not glamorous, but they cut setup time and prevent the slow drift that leads to out-of-spec parts. Over time, a well-worn fixture with penciled offsets and a few extra tapped holes becomes more valuable than the machine it sits on.
Reading the Shop Floor: User Feedback and Long-Term Reliability
Most reliability reports never capture what the night-shift operator mutters while resetting a fault for the third time. Those offhand remarks, logged informally or passed between shifts, often reveal more about a machine's true condition than a year of MTBF spreadsheets. When engineers spend time on the shop floor, they start to notice the small workarounds that operators invent: a folded shim under a sensor, a particular tap on a relay, a deliberate pause before cycling a pneumatic valve. Each one is a clue. Taken together, they map out where the documented process and the real process have drifted apart.
Long-term reliability is less about hitting a predicted failure curve and more about closing that gap. Machines that run for a decade do so because someone listened when a maintenance tech said the new bearing felt too hot, or when packing line workers pointed out that vibration had changed after a weekend rebuild. That kind of feedback rarely arrives through formal channels. It emerges in the break room, during walk-throughs, or when an operator says a machine has a 'new noise.' Respecting those observations, and acting on them quickly, keeps small annoyances from hardening into chronic breakdowns that no amount of scheduled servicing can undo.
Control Systems That Think Ahead of the Bend
A fast corner used to be a test of reflexes. Now the car gets a preview. Using map data, forward-facing cameras, and a constant stream of inertial measurements, the control system builds a short-term prediction of the road's curvature. Before the steering wheel moves much, it preloads the outside dampers, shifts torque to the rear axle, and tells the active anti-roll bars to expect a loading shift. The body stays flat not because it reacted, but because it was already braced.
The real trick is that the controller doesn't wait for error. Traditional stability control fires after yaw begins to deviate. A predictive system works the other way: it continuously compares the driver's inputs and the vehicle's current path against a moving horizon of what the road will demand. If the next 300 meters call for a tightening radius, the differential locks a little earlier, the steering ratio firms up, and the brake pads are pre-positioned. The interventions are so early they are almost invisible.
Inside the ECU, this runs as a model predictive control loop. Every few milliseconds it solves a constrained optimization—balancing speed, comfort, tire slip, and path tracking over the next two or three seconds. It then applies only the first slice of that plan before recomputing. The beauty is that the car feels calm. There's no sudden grabbing, no electronic panic. Just a chassis that already knows which way the road bends.
Material Handling and Workflow Integration: Where Efficiency Lives
On a busy warehouse floor, material handling is rarely just about moving boxes from point A to point B. It forms the physical rhythm of any operation, where every lift, turn, and placement either feeds the next step or creates a costly pause. Integrating these movements with the broader workflow means treating each transfer as a data point, not an isolated task. When a conveyor's speed adjusts to packing station demand, or a forklift's route is recalculated based on live order queues, the entire facility starts to breathe as one system.
Real gains appear when mechanized handling talks directly to production and inventory software. A palletizer that knows which boxes belong to a rush order can stage them for immediate pickup, while a shuttle system can hold back non-urgent totes without human direction. This two-way conversation eliminates the guesswork that typically clogs docks and staging areas. Operators spend less time hunting for the next task and more time fine-tuning exceptions, because routine decisions are made by the integrated flow itself.
The deepest form of this integration shows up in how smoothly disruptions are absorbed. A sudden spike in outbound orders, a late supplier truck, a machine fault—these stop being emergencies and become rerouting problems. Because material movement is bound to real-time workflow signals, the system can shift priorities across zones without idle chatter or manual whiteboards. Efficiency stops being a target metric and becomes the default behavior of a floor where every element—mechanical, digital, and human—knows what to do next.
FAQ
The difference usually shows up in frame rigidity, crowning system design, and how carefully they match the backgauge to the tooling. Average builders may hit a spec on a test sheet, but leaders consistently hold angular accuracy across a full shift as thermal growth and material variation kick in.
Don't just look at the brochure number for repeatability. Ask what happens after three hours of continuous bending on thick stainless steel. A meaningful precision figure is one that survives real thermal conditions, not just a cool machine at the demo.
Look at how the ram is guided, whether the crowning table adjusts automatically with load changes, and if the frame is stress-relieved after welding. Also check if the control software can compensate for material springback without requiring constant manual tweaks.
Request a live test on your own material or a close equivalent, not just their standard demo coupon. Measure the resulting angles at multiple points along the bend. Ask for data from an existing customer running similar parts for at least a year.
It's often the difference between a machine that loses precision within two years and one that stays consistent for a decade. Leaders tend to have local service engineers, clear documentation, and software updates that address real bending challenges rather than just adding features.
Try short, thick pieces where deflection is hardest to control, and long, thin pieces where crowning errors show up quickly. A builder that handles both without excessive shimming or manual correction usually understands structural design.
Strip away the brand story and ask for the machine's weight, frame construction method, and the type of hydraulic or electric drive. Compare those directly across candidates. Also run the same part program on each machine under time pressure and see which one needs fewer corrections.
Not always, but often the price reflects things you can't easily retrofit: a heavier frame, better crowning control, and a support network that keeps the machine accurate. If your parts have tight tolerances or high mix, that upfront difference tends to shrink over the machine's life.
Conclusion
Spotting a genuinely top-tier press brake builder means looking past glossy brochures and nominal tonnage figures. The real test happens on the shop floor, where repeated bends in high-strength or varying-thickness stock reveal whether a machine holds angular consistency across an entire shift. Industry leaders invite you to run your own parts before purchase, because they know their frames, crowning systems, and backgauges deliver repeatability that spec sheets can't fully capture. But a machine is only as good as what comes after it lands in your facility. The strongest manufacturers back their equipment with responsive field engineers, readily available spare parts, and training that goes beyond a quick handoff. Over time, user feedback from busy job shops tells a clearer story: machines that keep holding tolerance at year five or seven—with minimal unplanned downtime—are the ones worth the investment.
Leadership in precision bending also shows up in custom tooling and adaptive engineering. Instead of forcing your parts to fit a standard setup, leading builders modify clamping, punch holders, or backgauge fingers to match unusual profiles or tight flange lengths. Their control systems are equally forward-looking: offline programming, automatic angle correction, and real-time material springback compensation reduce trial bends and scrap. At the same time, efficient material handling and workflow integration separate true production partners from standalone machine sellers. Whether it's robotic loading, sheet followers, or seamless ERP connectivity, the best manufacturers design around how metal actually flows through your shop. When all these elements align—proven accuracy, dependable support, adaptable engineering, smart controls, and smooth material movement—you've found an industry leader, not just a vendor with an impressive data sheet.
Contact Us
Contact Person: Jeanie
Email: [email protected]
Tel/WhatsApp: +86 19805122954
Website: https://www.jianmeng.com